Company News

News
Company News Product News Exhibition activities
Company News

Company News

Who Ultimately Bears the Cost of a Rush Order?
2026.11.16
Who Ultimately Bears the Cost of a Rush Order?
Ask "can it be any faster" and the answer is almost always "we'll try." But who ultimately bears the cost of that "we'll try"? Mould production scheduling is not a straight line — it is four chains (design, procurement, machining, trial moulding) running in parallel and waiting to converge. A rush order doesn't accelerate one chain; it re-arranges the convergence point of all four: move yours forward an inch and someone else's project moves back an inch.
Three hidden time-killers that never appear on the lead-time sheet: ① no one signs the drawing, so machining won't start; ② the material grade is "TBD," so purchasing can't place the order; ③ parts come off the trial mould, but the sample approver isn't present.
A rush order is not free. Displace someone else today and your project gets displaced next time. What purchasing can bring forward is not machining speed but the decision point — freeze the drawing a week earlier and all five downstream links move forward together.
One line: lead time is not chased out; it is scheduled out. Jingmu reports scheduling status at each project node and flags the risk while the drawing is still unfrozen — handing the choice back to the customer.
Cooling Is Not Just Drilling a Few Holes: 4 Variables in a Mould Cooling Design
2026.11.14
Cooling Is Not Just Drilling a Few Holes: 4 Variables in a Mould Cooling Design
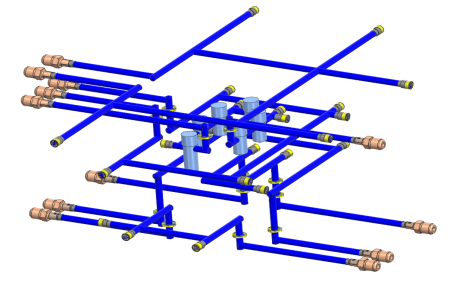
Cooling is decided at the design stage; trial moulding can only fine-tune it. When the cycle won't come down or a multi-cavity part warps, the cause is often cooling lines at uneven distances from the cavity surface and moving/fixed halves without zoned temperature control — the temperature difference only surfaces after heat accumulation. Four variables decide whether heat is removed evenly: ① cooling-line layout vs. cavity surface governs uniformity; ignore it and warpage appears after continuous running; ② zoned temperature control & circuits manage the moving/fixed half temperature difference, avoiding uneven shrinkage; ③ temperature measurement records must contain measuring-point location, moving/fixed half readings, steady-state data, batch & machine, recorder & time — recording only the first shot amounts to not measuring at all; ④ maintainability — missing cleaning ports and maintenance intervals lead to scaling, and the cycle lengthens month by month. Chain reaction of uneven mould temperature: local hot spots stretch the cycle, cause warpage, and for thermoset materials produce inconsistent degrees of cure. Three mass-production observation points: the cycle lengthens under the same parameters, inter-cavity variation grows, flow drops while TCU load rises — check scaling first, not injection parameters. Priorities by product type: thin-wall parts → cooling-line layout vs. cavity surface; multi-cavity parts → symmetry & zoning; thermoset parts → temperature uniformity & thermocouple placement; high-gloss parts → moving/fixed half temperature difference & steady-state records. At the review, tick the type first and treat the corresponding row as a mandatory check item. Jingmu delivers cooling solutions and records by product type, retains steady-state measured data, and supports the corresponding reviews and verifications.
How Was That
2026.11.13
How Was That "Conforming" Dimension on the Report Actually Measured?
Inspection data is not "read off" — it is produced under conditions of equipment, environment, datum, clamping, and acceptance rules. Disputes are rarely about whether the data is true or false, but about conditions not being written into the agreement. Key variables: ① measurement equipment & method; ② gauge calibration; ③ measurement environment (temperature, thermal equilibration); ④ datum & measuring-point definition; ⑤ acceptance rules (drawing revision, dimension list). For thin-wall parts, extra attention to clamping deformation, measurement timing, and contact vs. non-contact differences. "Comparable" matters more than "conforming": achieve the "three consistencies" — same datum & measuring points, same measurement method, same acceptance rules. Before changing the gauge, the operator, or the environment, first run a correlation with a comparison sample. Four-step check when re-inspection disagrees: check drawing revision → check datum, measuring points & clamping → check equipment, calibration & environment → only when the first three are consistent do we discuss re-measurement or concession acceptance. Eight required report fields: mould no./cavity no., part information, drawing revision, dimension list & tolerances, measured values, equipment & calibration, environmental conditions, inspector/date/conclusion. Three actions for purchasing & quality: before mould making, write key dimensions, datum & measuring points into the technical agreement; attach equipment, calibration, environment & drawing revision to the report under a unified template; in mass production, fix measuring points for trend records and retain comparison samples. Jingmu's commitment:​ first-article full inspection and records per the agreed datum & measuring points, archived against the mould number; correlation and record updates whenever the revision or measurement method changes.